Upgrade your high-performance 3D printer with the Wham Bam Flexi Plate with Carbon Fiber, specifically sized at 355 x 355 mm. Engineered with authentic 3K woven carbon fiber panels factory-bonded to a high-flex spring steel plate using high-temperature 3M adhesive, this top-of-the-line build surface delivers incredible durability, heat resistance, and effortless print release.
Because the thermoset polymer carbon composite cures through a chemical process, it will not re-melt or over-bond with high-temperature or aggressive materials like PETG, ASA, PEI, or PEEK—making it the ideal smooth surface alternative to standard PEI or PEX plates.
Key Features & Specifications
-
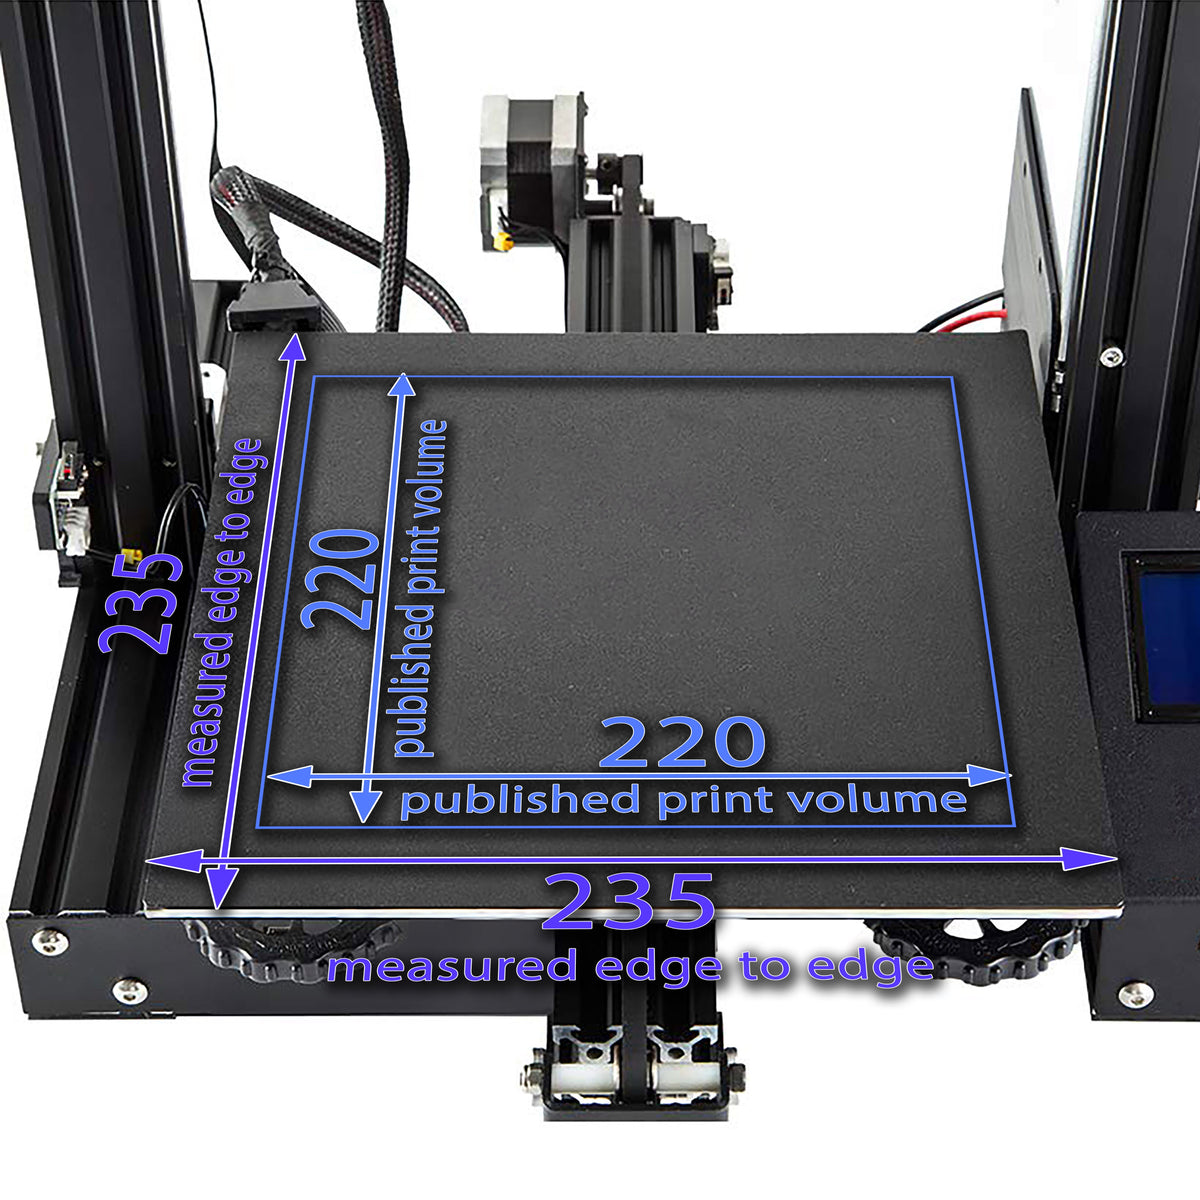
Dimensions: 355 mm x 355 mm
-
Plate Thickness: 0.4 mm high-flex spring steel core
-
Build Surface Thickness: 0.4 mm authentic woven carbon fiber panel
-
Surface Finish: Extremely smooth finish with a subtle cross-light woven pattern (not an effect/imitation sheet)
-
Package Includes: 1x Flexi Plate with pre-applied Carbon Fiber Build Surface
Printer Compatibility
Direct Fit:
- Sovol SV08
- VORON Design 350 V2
May Fit (Check Dimensions):
Setup, Maintenance & Best Practices
Note: A high-temperature magnetic base is required to secure the Flexi Plate to your heated bed. Carbon fiber is electrically conductive and acts as a magnetic shield; this plate is strictly designed for single-sided use.
Initial Surface Preparation & Cleaning
Before first use, thoroughly clean the build surface with >90% Isopropyl Alcohol (IPA) using a clean paper towel (avoid microfiber or shop rags). Alternatively, wash with warm water and strong dish soap to eliminate surface oils and fingerprints.
Bed Leveling & Thermal Guidelines
Re-level your bed after installation. For probe/touch leveling systems, maintain nozzle temperatures under 140°C during probing to protect the surface from physical marking. Keep first-layer hot-end temperatures at or below 270°C. Pre-heating the bed (50–70°C for standard materials) for ~5 minutes prior to printing ensures optimal bed adhesion.
Part Removal & Adhesives
Allow the surface to cool fully for automatic or low-effort part release. Use adhesion promoters (e.g., Vision Miner Nano Polymer, Magigoo, Glue Stick) when printing warping-prone materials such as ABS or Nylon in enclosed environments.
Downloads & Resources